 Search

A hydraulic vane pump may appear relatively simple from the outside, yet considerable mechanical and fluid-dynamic activity takes place inside its housing. As pressure rises, the rotor turns continuously, vanes slide through their slots, and the pumping chambers repeatedly expand and contract. Every rotation creates a series of pressure and contact changes that influence flow stability, internal leakage, friction, and component loading.
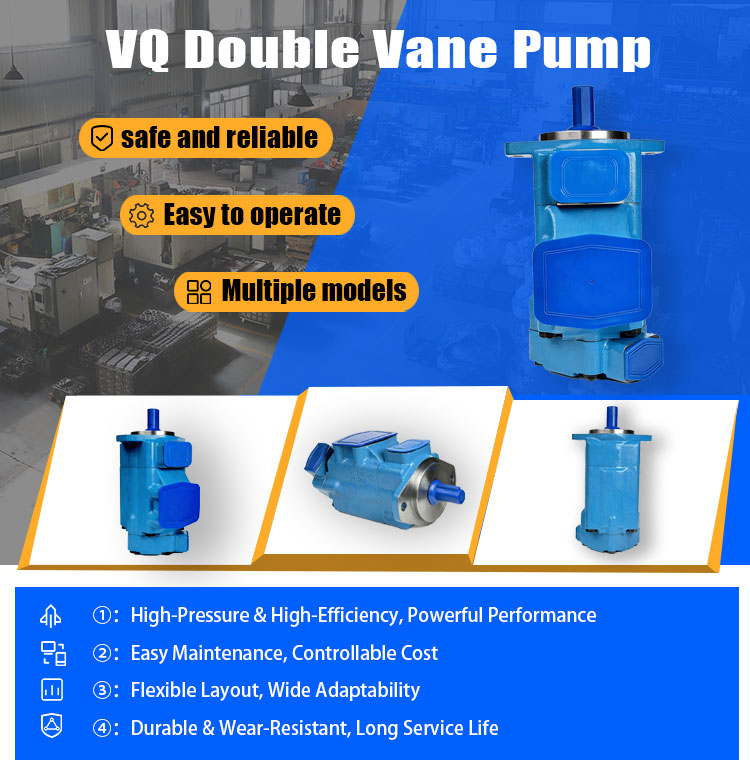
For demanding machinery, understanding these internal processes is useful when evaluating a Heavy Duty Hydraulic Vane Pump. The external pressure rating tells only part of the story. The internal cartridge, vane geometry, cam ring, pressure plates, shaft, and clearances all contribute to how the pump behaves under sustained hydraulic loads.
The Rotor Is Only Part of the Pumping Action
At the center of a vane pump is a slotted rotor connected to the drive shaft. Several vanes sit inside the rotor slots and move radially as the rotor rotates inside the cam ring.
- Rotor: Transfers mechanical rotation from the drive shaft to the vane assembly.
- Vanes: Divide the internal space into individual pumping chambers.
- Cam ring: Controls the radial movement of the vanes as the rotor turns.
- Pressure plates: Form the sides of the pumping chambers and help control internal clearances.
- Housing: Contains the cartridge and directs hydraulic fluid through the inlet and outlet passages.
Research on balanced vane pumps describes the cartridge as a combination of rotor, cam ring, vanes, and pressure plates. As the rotor turns, the vanes move outward and inward according to the cam-ring profile, creating changing chamber volumes that produce the displacement action.
What Happens During One Rotation?
The pumping cycle can be understood through changes in chamber volume. As a vane moves through the inlet region, the chamber behind it increases in volume. This creates the conditions required for hydraulic fluid to enter the chamber.
As rotation continues, the chamber moves toward the outlet side. The available volume decreases, forcing the trapped fluid toward the discharge port.
| Rotor Position | Chamber Condition | Hydraulic Action |
|---|---|---|
| Inlet region | Volume increases | Fluid enters the chamber |
| Transition zone | Volume reaches its working range | Fluid is carried by the rotating vane |
| Outlet region | Volume decreases | Fluid is displaced toward the outlet |
| Return to inlet | Cycle repeats | New fluid enters the chamber |
This repeated expansion and contraction occurs continuously while the shaft rotates. A properly designed vane profile helps maintain separation between adjacent chambers while controlling the contact forces between the vane tips and cam ring.
Why Vane Tip Contact Matters
The vane tip has a demanding job. It needs to maintain sufficient contact with the cam ring to prevent excessive fluid bypass, yet excessive contact force can increase friction and wear.
This creates a delicate balance inside a Heavy Duty Hydraulic Vane Pump. Hydraulic pressure acts on the vane, while centrifugal force and other loading mechanisms influence its position. At the same time, the vane slides along the cam-ring surface at high speed.
Research into high-pressure balanced vane pumps shows that vane position and tilt can change during operation. These movements affect the vane-to-cam-ring interface and can influence both volumetric performance and frictional losses.
Too Little Contact
A vane that loses effective contact with the cam ring can create a leakage path. Under high-pressure conditions, this can become particularly significant because pressurized oil can move through internal clearances rather than remaining within the intended pumping chamber.
Too Much Contact
Excessive loading at the vane tip increases sliding friction. Over time, this can affect the vane, cam ring, and associated cartridge components.
The engineering challenge is therefore to maintain an appropriate contact condition throughout the rotation rather than simply applying greater force to the vane.
How Pressure Balance Changes Internal Forces
Balanced vane pump architecture is particularly interesting under high-pressure operation. Symmetrical porting can counteract radial hydraulic forces acting on the rotor. Research on balanced vane pumps notes that this pressure symmetry produces no net radial load on the rotor in the ideal balanced configuration, making the design suitable for high-pressure applications.
This principle is important because hydraulic pressure does not only create useful output force. It also creates internal mechanical loads. A pressure-balanced design distributes these forces more evenly around the rotating assembly.
Commercial high-pressure vane pump designs apply this concept in different ways. Danfoss, for example, describes pressure-balanced vane construction as a method of reducing flow pulsations and noise while supporting service life. Its V20H series provides continuous pressure ratings up to 205 bar, while other high-pressure square vane configurations are designed around demanding mobile and industrial applications.
Where Does Internal Leakage Occur?
Hydraulic pumps require controlled internal clearances. These clearances allow components to move while limiting unwanted oil flow. Under pressure, however, even a small clearance can become a leakage route.
Research identifies several important interfaces inside a balanced vane pump:
- Rotor-to-plate interface
- Vane-to-plate interface
- Vane-to-rotor interface
- Vane-to-cam-ring interface
Among these interfaces, the rotor-plate and vane-plate regions are identified as important internal leakage paths. The vane-cam-ring interface also has a strong relationship with vane motion, friction, and volumetric behavior.
High Pressure Makes Clearances More Important
Imagine a pump operating at 200 bar. The hydraulic pressure difference across an internal clearance can be substantial. Even though the gap may be extremely small, pressurized oil can pass through it continuously.
This is why the internal geometry of a Heavy Duty Hydraulic Vane Pump requires careful control. The goal is not to eliminate every clearance, because moving components need controlled working gaps. Instead, manufacturers must establish clearances that balance lubrication, thermal expansion, mechanical movement, and leakage control.
| Internal Area | Main Function | Potential Concern Under Heavy Load |
| Vane tip / cam ring | Separates pumping chambers | Friction, wear, leakage |
| Rotor / pressure plate | Controls side clearance | Internal leakage |
| Vane / rotor slot | Allows radial vane movement | Friction and restricted movement |
| Shaft / bearing system | Supports rotating assembly | Mechanical loading |
Why Speed Changes the Internal Picture
Pressure is not the only factor affecting a vane pump. Rotational speed also changes what happens inside the cartridge.
At higher RPM, the vanes move rapidly through the cam-ring profile, increasing the frequency of contact and pressure cycles. At very low speed, however, centrifugal loading becomes weaker. This can create another challenge under high pressure because vane contact may become less stable.
A 2026 study investigating balanced vane pumps under ultra-low-speed and high-pressure conditions reported that conventional vane structures can experience reduced volumetric performance and increased leakage at very low rotational speeds. The research examined operation below 500 rpm and reported a test condition of 100 rpm and 21 MPa where a spring-assisted vane design maintained flow while a conventional pin-loaded configuration experienced vane detachment.
This finding highlights an important product consideration: a pump designed for high pressure at normal operating speed may face different internal challenges at very low speed.
What Heavy-Duty Construction Really Means
The phrase “heavy duty” should not be interpreted simply as a thicker pump housing. A demanding vane pump involves several interacting design elements.
- Pressure-balanced cartridge: Helps manage radial hydraulic loading.
- Vane geometry: Influences contact force, sealing behavior, and sliding motion.
- Rigid housing: Helps maintain cartridge alignment under operating loads.
- Controlled clearances: Balance lubrication requirements against internal leakage.
- Bearing arrangement: Supports the rotating assembly and transfers mechanical loads.
- Material selection: Determines resistance to pressure, friction, temperature, and fluid conditions.
Parker's T7 vane pump documentation, for example, describes balanced construction and double-lip vane technology alongside high-pressure and high-speed capability. Its published data includes double-pump configurations with displacement options ranging from approximately 21.6 to 200 cm³/rev for a listed T6CCM series.
What Buyers Should Look Beyond the Pressure Rating?
A specification such as “250 bar” or “3000 psi” provides useful information, but it does not describe the entire operating envelope of a pump.
Equipment designers should also examine:
- Displacement in cm³/rev
- Continuous and intermittent pressure
- Permitted rotational speed
- Fluid viscosity range
- Maximum fluid temperature
- Shaft and mounting configuration
- Cartridge construction
- Inlet conditions and allowable suction characteristics
Parker's vane pump documentation specifically recommends checking speed, pressure, temperature, fluid quality, viscosity, rotation, inlet conditions, shaft capability, coupling alignment, and filtration as part of application evaluation.
The Internal Design Defines the Real Working Character
A Heavy Duty Hydraulic Vane Pump is effectively a coordinated system of moving surfaces, pressure chambers, controlled clearances, and load-balancing structures. The rotor generates motion, the vanes divide the pumping chambers, and the cam ring determines their changing volume. At the same time, pressure forces act on the cartridge while thin oil films help separate moving surfaces.
Under demanding conditions, small changes in vane position, clearance, pressure, or rotational speed can influence the entire pumping process. This is why two pumps with similar external dimensions and identical nominal pressure ratings can behave differently in actual machinery.
Final Takeaway
The real story inside a heavy-duty vane pump is a continuous interaction between pressure, rotation, vane movement, sealing, lubrication, and mechanical loading. High-pressure performance depends on more than the strength of the housing. The internal cartridge and its ability to maintain controlled contact and balanced forces are equally important.
For hydraulic equipment designers and buyers, examining these internal characteristics can provide a clearer understanding of what a Heavy Duty Hydraulic Vane Pump can actually deliver. Pressure rating establishes a boundary, but rotor geometry, vane design, pressure balancing, internal clearances, speed capability, and material construction determine how the pump behaves inside that boundary.
